How to Weld Sheet Metal
Thin sheet metal needs tight fit-up and deliberate heat control. A long continuous bead that works on thicker steel can distort a panel or burn through its edge. Start with scrap of the same material, thickness and joint rather than practising on the finished panel.
Make the joint easier before changing settings
Trim accurately, remove contamination and support the pieces so their edges remain aligned. A gap that changes along the seam changes the welding problem as you travel. Check both faces for hidden paint, seam sealer or other coatings before heating.
A controlled sequence for practice
| Stage | Purpose |
|---|---|
| Fit and clamp | Hold alignment without forcing a distorted panel flat |
| Place tacks | Stabilize the joint before filling the seam |
| Inspect alignment | Correct movement while the joint is still accessible |
| Add short welds in a planned sequence | Limit concentrated heat buildup |
| Allow cooling and reassess | Avoid chasing distortion with more heat |
Miller's sheet-metal demonstration uses short stitching with cooling instead of one uninterrupted seam. Its settings belong to that demonstration and equipment, not every panel. Use your machine's thin-material guidance and compare matching test pieces.
Choose a process for control
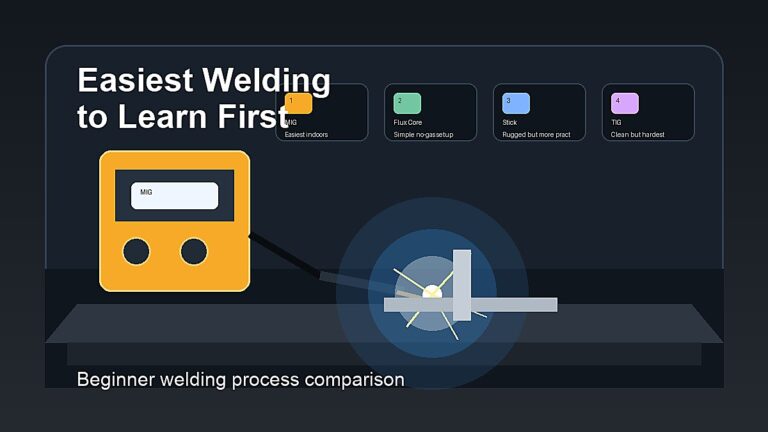
Solid-wire MIG and TIG can both be used for suitable thin-sheet jobs. The machine's minimum useful output and arc behavior matter. Self-shielded wire is not automatically interchangeable: check its specified thickness range before trying it on a delicate panel.
Practice grinding separately. Aggressive cleanup can thin the parent sheet even when the weld itself was acceptable. Inspect before grinding away the profile, and avoid heating the panel heavily during finishing.
Why does turning the welder down not always stop burn-through?
Poor fit-up, excessive dwell and repeated heating can still melt the edge. A cold deposit can also conceal poor fusion. Fix the joint and sequence as well as the parameters.
Can this guide be used for structural automotive repairs?
No. Vehicle structures may use special alloys, coatings and manufacturer repair procedures. A cosmetic practice panel is not evidence that a safety-critical automotive weld is acceptable.
Continue learning
Sources and limits
This is an educational reference. Follow the exact equipment and consumable instructions; safety-critical welding needs appropriate qualifications, procedures and inspection.