Flux Core Welding for Beginners
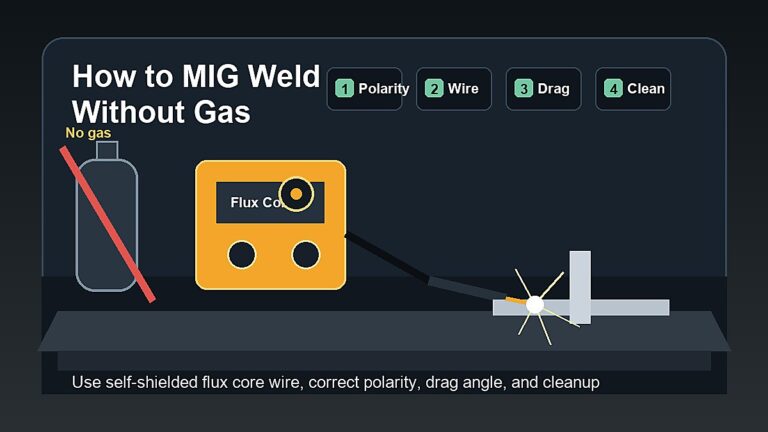
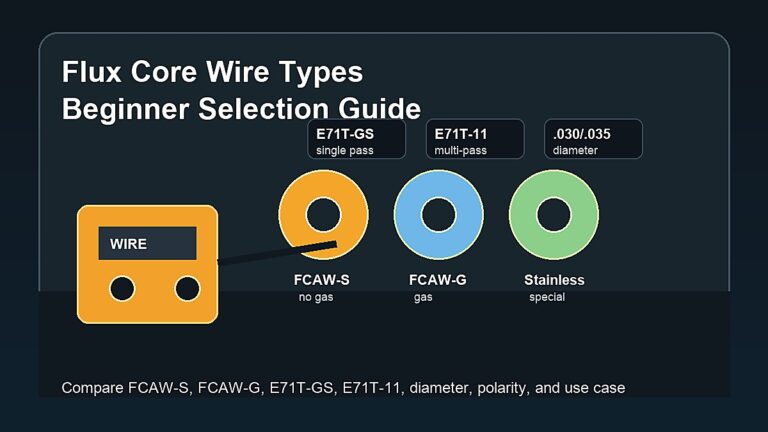
Self-shielded flux-core welding uses tubular wire whose flux provides shielding. It does not require an external gas cylinder, but it still creates fumes, spatter and slag. Gas-shielded flux-cored wire is a different consumable and does require the specified gas.
Confirm the wire before switching the machine
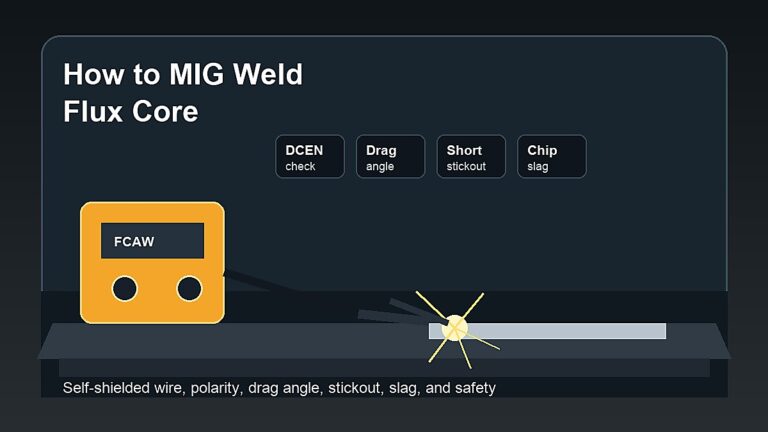
Read the wire classification, diameter, polarity and permitted thickness/position range. Many common small self-shielded steel wires use electrode negative, but the label is the authority. Do not leave the machine in a solid-wire MIG configuration simply because the gun looks the same.
Check drive-roll suitability, tip size and wire feeding. Apply enough tension to feed steadily without crushing the wire. With power isolated as the manual directs, inspect feeding problems before changing welding settings.
Practice with slag in mind
| Stage | Useful beginner check |
|---|---|
| Before the arc | Clean identified steel, fitted joint, correct polarity and ventilation |
| During the run | Use the wire manufacturer's specified extension and travel technique |
| Between passes | Remove slag completely and inspect corners |
| After cleaning | Look for pores, undercut and poor tie-in before continuing |
For many slag-forming self-shielded applications a drag technique is appropriate; follow the wire instructions rather than transferring a solid-wire MIG habit. Use a short practice joint where you can keep the pool visible. A longer bead is not progress if you lose control halfway through it.
Do not mistake portability for unrestricted outdoor use
Wind resistance does not make the process fume-free or fire-safe. Check where sparks can travel and how fumes leave the breathing zone. Outdoor welding can still need exposure controls. Unknown coatings and sealed containers are unsuitable practice material.
Can I put shielding gas on self-shielded wire to improve it?
Do not improvise a shielding combination. Use the wire under its specified conditions or change to a consumable designed for the intended process.
Why does the bead look different after chipping?
The visible surface during cooling may be slag rather than weld metal. Remove it before assessing the bead or laying another pass. A tidy slag cover does not demonstrate fusion underneath.
Continue learning
Sources and limits
This is an educational reference. Follow the exact equipment and consumable instructions; safety-critical welding needs appropriate qualifications, procedures and inspection.