Spot Welding Parameters Chart for Uncoated Steel
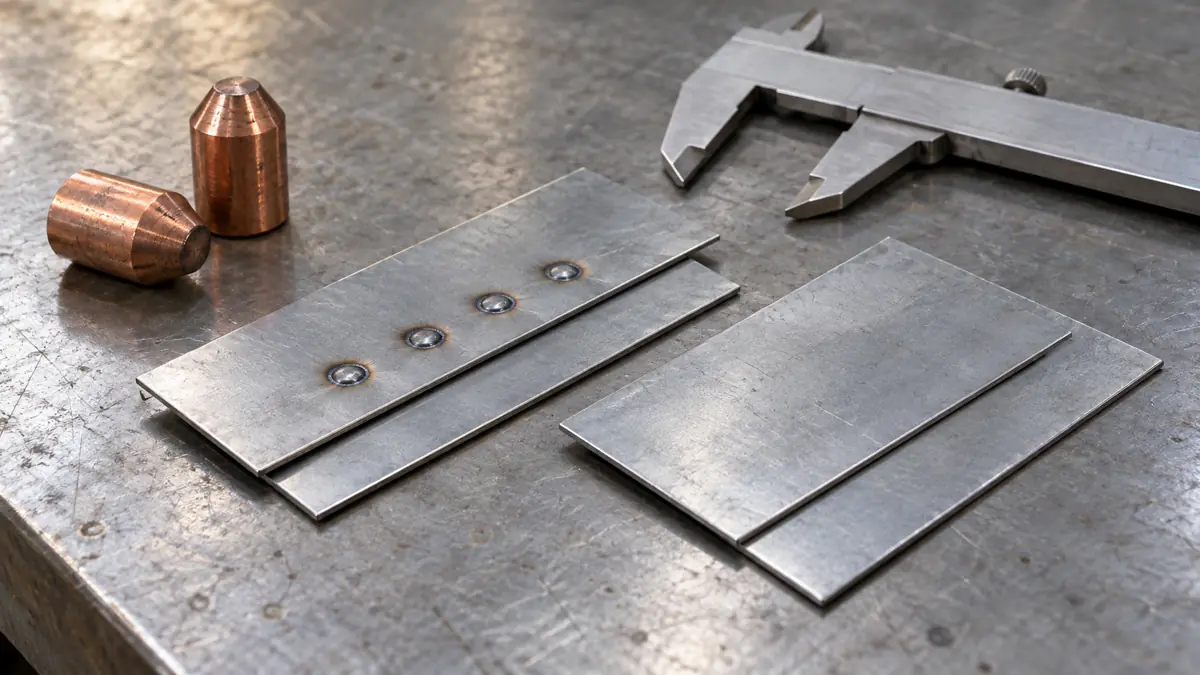
A useful spot welding parameters chart keeps sheet thickness, electrode tip size, force, current and weld time together. A current figure without those conditions is not a complete setup. The selected examples below apply to uncoated low-carbon steel sheet and are starting references for process development, not automatic approval for a production joint.
If you are new to resistance spot welding, first understand how the electrodes clamp overlapping sheets and form a nugget between them. Our spot-welding introduction explains the process. This article focuses on reading a numeric schedule and deciding what must be checked before a trial.
Selected chart: uncoated low-carbon steel sheet
PW Resistance Welding Products publishes typical conditions and identifies its data source as BS EN ISO 14373:2015. The excerpt below uses only its medium-force, long-time group. These are selected thickness bands, not the supplier’s entire table.
| Single-sheet thickness band (mm) | Electrode tip diameter (mm) | Force (kN) | Weld time (cycles) | Current (kA) |
|---|---|---|---|---|
| Over 0.4, up to and including 0.6 | 4 | 0.9–1.1 | 5–7 | 4–6 |
| Over 0.8, up to and including 1.0 | 5 | 1.4–1.5 | 9–12 | 6–8 |
| Over 1.2, up to and including 1.6 | 6 | 1.9–2.1 | 14–18 | 8–11 |
Timing note: the source defines one cycle as 0.02 seconds. Keep that convention attached to this chart. Its thickness column refers to a single sheet, not the sum of every layer in the stack.
For missing thickness bands, another material or a different welding-condition group, consult the complete source and the applicable procedure. Do not interpolate a setting from two convenient rows or claim that this excerpt reproduces all requirements of a standard.
Read one row before selecting any numbers
Consider a 1.0 mm single-sheet thickness. It belongs to the band that ends at and includes 1.0 mm. Read across that row as a linked set of conditions. Do not move to another band because the current looks closer to a machine’s preferred setting.
The range entries also need interpretation within a development plan. They do not prove that every combination of minimum and maximum values produces an acceptable weld. Verify a suitable schedule on the identified material and assembly.
A practical transcription habit is to keep the whole source row beside the trial record. Entering “6–8” into a notes box without “kA” loses information that the next person needs.
Check the timing convention on the control
For the chart’s stated convention, nine cycles is 180 ms and twelve cycles is 240 ms. That is arithmetic based on 0.02 seconds per cycle. It does not mean a value of nine entered into any controller gives the same duration.
A different supplier’s SAE 1005–1010 setup guide explicitly uses 60 Hz cycles, inch dimensions and force in pounds. Its schedule groups also carry their own context. Preserve those details rather than combining columns from different charts.
Read your control’s manual for its actual units, timing basis and pulse sequence. In a multi-pulse schedule, current-on intervals, cooling intervals and total elapsed sequence time are different quantities.
Separate squeeze, weld and hold
The ENTRON EN1000/EN1001 manual describes separate sequence functions. Squeeze allows the electrodes to close and force to establish. Weld/heat is the current-flow interval. Hold follows welding while the electrodes remain in contact as the joint solidifies.
Record each required stage. A chart that gives a weld duration has not necessarily told you the squeeze or hold values for your machine. Increasing one is not a substitute for correcting another.
The manual also distinguishes percentage-current programming and constant-current operation. Do not convert a percentage display into kiloamps by assuming the scale is linear or identical across equipment.
Confirm the sheet stack and surface condition
Record every layer’s material, thickness, coating and orientation. Two matching uncoated sheets, an unequal stack and a coated assembly should not be treated as equivalent because their total thickness happens to match.
For coated steel, TWI explains that the coating changes the required conditions and electrode behavior. Zinc-coated work commonly needs different current and force from comparable uncoated sheet, and coating interaction can increase electrode wear.
Use coating-specific guidance rather than adding an arbitrary percentage to the chart. If the part has an unfamiliar coating, adhesive or surface treatment, establish its identity and the required joining and exposure controls first.
Keep the electrode condition in the record
The table includes tip diameter for a reason. Electrode wear, alignment, cooling and surface condition are part of the process, not details to inspect only after failures begin.
TWI’s electrode-wear guidance discusses cooling, suitable operating conditions and electrode maintenance. Follow the tooling supplier’s dressing or replacement instructions and verify the restored geometry.
If the process starts drifting, compare the current tool condition with the recorded one before chasing settings. A schedule developed with one contact face should not quietly be treated as validated after the tooling has changed.
A trial sheet that keeps the important information visible
WeldingPilot chart note: label the first column “source reference” and the second “trial setting.” Leave the approval field blank until the required review has actually occurred.
| Record | Include |
|---|---|
| Joint identity | Part drawing, stack order, sheet grades, individual thicknesses and coatings. |
| Equipment and tooling | Welder, control, program, electrode material, geometry, condition and cooling arrangement. |
| Schedule | Force, current, timing units, squeeze, weld, hold and any additional stages. |
| Verification | Measured process values, sample identity, test method, results and acceptance requirement. |
| Decision | Reviewer, revision, approved scope and any further work required. |
Change variables under a controlled plan and keep rejected samples identifiable. Record what happened rather than replacing an unsuccessful result with the next good one. That history helps distinguish a repeatable process from an isolated acceptable sample.
Verify the weld and the application
A circular electrode impression is not proof of an acceptable internal nugget. Set the required inspection and test method before trials, including the criteria for nugget size, mechanical performance or other application requirements.
Use the relevant procedure for destructive samples and any additional examination. Avoid adopting a familiar rule of thumb as a universal release criterion. Vehicle, pressure and other specified applications may impose requirements beyond a general sheet-steel chart.
Also distinguish resistance spot welding from making an arc-welded plug or placing a short MIG tack. Our stick-welder and spot-welding comparison explains that equipment/process distinction. A resistance schedule cannot simply be entered as arc-welding settings.
Use suitable guarding, electrical protection and safe setup procedures. Keep hands out of the closing electrode area and isolate equipment appropriately for servicing. OSHA’s resistance-welding requirements address guarding and equipment protection.
Frequently asked questions
Should I use total stack thickness in this table?
No. This excerpt preserves the supplier’s single-sheet thickness column. Obtain appropriate guidance for your actual layer combination rather than substituting the total.
Can I use it for battery tabs or aluminum?
No. The selected conditions concern uncoated low-carbon steel sheet. Other materials, thin tabs, power sources and electrode arrangements need their own applicable information.
Does matching the chart mean the weld is approved?
No. Matching reference values is not a substitute for a verified schedule, correct equipment condition and the inspection and acceptance requirements of the job.